Standard & Custom Stator Processing Equipment
Engineered in our Dongguan facility and customized for 400V/50Hz CE-compliant European shop floors. Choose from individual forming stations to complete automated winding and inserting cells.

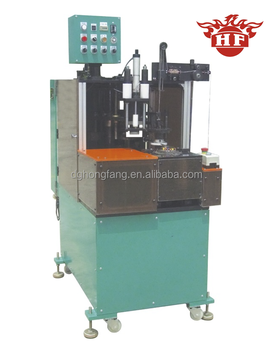
HONGFANG HF-D50 Green Insulation Paper Insertion Machine
- Power: 220V/380V, 1000W Servo Control
- Auto Creasing, Sizing & Slot Insertion
- 1-Year Comprehensive Warranty

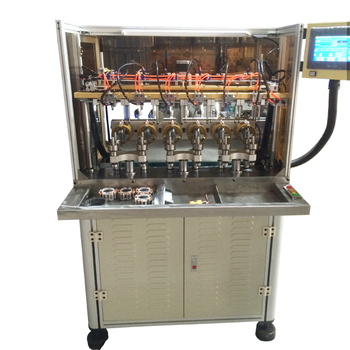
Electrical Motor Stator Coil Winding Machine
- High-Speed Multi-Pole Stator Coiling
- Copper & Aluminum Enamelled Wire
- Microprocessor Loop Regulation

Motor Stator Coil Forming & Shaping Machine
- Hydraulic Preforming & Final Sizing
- Precise Internal/External Flare Control
- 1 kW High-Rigidity Forming Dies

Slot Paper Inserting & Cutting Machine
- Multi-Slot Table, Pump & Fan Motors
- Configurable 380V / 220V Dual Voltage
- Hardened High-Speed Steel Blades

Two Stations Motor & Transformer Coil Winding
- Dual Synchronized Turntable Spindles
- External Stator Coiling Capability
- Independent Station Tension Control

2-Station Outer Stator Coil Winding Machine
- External Flyer Winding for BLDC & Steppers
- High Efficiency Dual Station Turnover
- Programmable Layering Trajectories

Fully Automatic Motor Coil Winding Machine
- Continuous High-Speed Coil Formation
- Multi-Strand Wire Compatibility
- Integrated Lead Wire Terminal Trimming

Hydraulic Stator Shaft Inserting Press Machine
- Controlled Hydraulic Force Profiling
- Zero-Eccentricity Core Centering Guides
- 1-Year Structural & Valve Warranty
Poznań as Poland's Strategic Electromechanical Center
The Greater Poland (Wielkopolska) Voivodeship, centered on Poznań and industrial corridors such as Swarzędz, Tarnowo Podgórne, Komorniki, and Września, represents one of Central Europe's most dynamic clusters for automotive Tier-1 manufacturing, electric vehicle traction drives, and advanced ventilation equipment.
With major automotive production plants, specialized motor suppliers, and HVAC system makers established along the A2 trans-European transport corridor, Poznań manufacturers face continuous pressure to improve stator slot fill factors, eliminate insulation abrasions, and reduce cycle times while upgrading to strict European IE4 and IE5 energy efficiency directives.
Stator coil preforming is the defining intermediate process that governs the final electrical integrity and geometry of AC induction motors, permanent magnet synchronous motors (PMSM), and brushless DC (BLDC) units. Zunqi Intelligent Equipment bridges direct Asian machine tool manufacturing with the exacting engineering standards required across Poznań's precision automation sector.



The Mechanics of High-Density Stator Coil Preforming
Why modern high-efficiency motors require multi-stage hydraulic and servo-assisted end-turn profiling to prevent phase insulation breakdown and preserve electromagnetic air gap uniformity.
End-Turn Flare Sizing
After automated coil insertion, copper end-windings flare outward and inward irregularly. A specialized preforming press expands the inner diameter to guarantee rotor insertion clearance while simultaneously compacting the external perimeter within strict motor frame boundary envelopes without scuffing the enamel coating.
Slot Wedge Locking & Crease Protection
During preforming, axial expansion forces must be calibrated to avoid dislodging DMD, Nomex, or polyester slot liners. High-precision segmented forming shoes distribute radial pressure evenly across all teeth, securing phase isolation paper deep inside the slot shoulder before final binding and lacing cycles.
Electromagnetic Fill Factor Gain
Preforming machines permit higher initial wire counts to be loaded into each slot. By pre-compressing intermediate coil passes, machine operators can achieve total slot copper fill factors exceeding 75%, directly enabling EU EcoDesign Regulation 2019/1781 compliance for IE4 super-premium efficiency drives.
Stator Coil Processing: Preforming vs. Conventional Shaping
Review the technical distinctions between multi-stage intermediate preforming and archaic manual shaping methods commonly observed in non-automated workshops.
| Evaluation Parameter | Zunqi Automatic Stator Preformer | Conventional Manual / Pneumatic Shaping | Operational Benefit in Poznań Factories |
|---|---|---|---|
| Axial Dimensional Tolerance | ±0.25 mm repeatable height regulation | ±1.8 mm to ±3.0 mm variable variance | Guarantees motor end-shield clearance without interference fit issues. |
| Coil Flare Concentricity | Segmented multi-jaw expanding mandrel (≤0.08 mm) | Single-cylinder manual press blocks | Eliminates stator-rotor air gap rubbing in compact PMSM designs. |
| Cycle Time Per Stator | 6 to 12 seconds per cycle (two-end simultaneous) | 45 to 90 seconds (manual multi-step mallet/press) | Substantially cuts labor overhead for serial automotive batch runs. |
| Enamelled Wire Preservation | Hard-chromed, polished tool steel dies (Ra ≤ 0.2 μm) | Standard mild steel or composite blocks | Prevents micro-fissures, corona discharge, and inter-turn short circuits. |
| Control Architecture | Siemens / Delta / Mitsubishi PLC + Touch HMI | Relay logic or foot-pedal mechanical actuation | Supports recipe storage for rapid stator stack and ID changeovers. |
Where Zunqi Preforming Equipment Excels in Wielkopolska
Targeted industrial production scenarios across the Poznań-Września-Gniezno manufacturing triangle.
Electric Mobility & Auxiliary Motors
With Wielkopolska serving as a prime hub for commercial vehicles, EV buses, and sub-tier suppliers, our preforming stations process high-amperage cooling pump motors, power-steering drives, and electric brake actuators with zero wire insulation defect rates.
Industrial Fans & HVAC Blowers
Ventilation and cleanroom fan assembly lines in Poznań's logistics parks demand cost-competitive, high-volume production. Our automatic coiling, paper inserting, and coil forming combinations allow factories to transition effortlessly between single-phase and three-phase designs.
Hydraulic Submersible Pumps
Submersible deep-well pump motors demand flawless hermetic insulation. Preforming and lacing under uniform pneumatic-hydraulic parameters guarantees that end-windings undergo vacuum pressure impregnation (VPI) without creating internal air pockets or uneven resin distribution.
Precision Servo & Robotic Actuators
Factory automation rebuilds in central Poland frequently require compact, torque-dense multi-station stators. Our fine-tolerance forming dies handle condensed end-windings with slot numbers ranging from 8 to 48 slots, ensuring optimal air-gap alignment.

Technological Shifts Governing Polish Stator Lines
The manufacturing environment in Poland is undergoing rapid modernization driven by escalating labor costs, severe technician shortages, and mandatory EU carbon footprint targets. Production managers in Poznań and across Wielkopolska are phasing out standalone, operator-reliant shaping blocks in favor of integrated, data-traceable cells.
1. Strict Adherence to EU Ecodesign Directives: Standard IE2 and IE3 induction motors are rapidly being superseded by IE4/IE5 synchronous reluctance (SynRM) and PM architectures. These require tighter coil packing, thinner lamination sheets (0.35 mm to 0.2 mm), and zero mechanical shock during intermediate preforming.
2. Multilingual CE-Compliant Control Platforms: Machines supplied to Wielkopolska facilities must incorporate EN ISO 12100 safety mechanics, two-hand start interlocks, light curtains, and PLC control setups supporting Polish/English operator interfaces with local component interchangeability (Siemens S7-1200, Schneider Electric, or Omron).
3. Transition from Decentralized Supply to Single-Source Accountability: Polish OEMs now favor turn-key stator equipment providers capable of coordinating slot paper insertion, coiling, inserting, forming, and double-side lacing within a synchronized cycle time framework.
Why Polish Motor Makers Partner with Zunqi Intelligent
Direct manufacturer pricing, deep engineering customization, and 17+ years of international export pedigree.
Onsite Verified Facility
Based in Dongguan's Qishi Town industrial center, our manufacturing campus has undergone strict independent onsite verification. Buyers can review production licenses, assembly bays, credit histories, and machining centers directly via video and documentation.
Stator Tooling Tailored to Drawings
We do not provide generic off-the-shelf dies. Every preforming horn, expanding blade, and insertion finger is CNC-machined to your exact stator lamination CAD drawings, core stack height limits, and slot fill requirements.
Rapid Multilingual Support (≤9h)
With an average technical inquiry turnaround under 9 hours, our senior mechanical and electrical engineers work directly with European plant maintenance directors to supply circuit schematics, remote video diagnostics, and air-freight spare parts.
Questions Polish Industrial Engineers Ask Before Ordering
Clear answers covering European electrical compliance, logistics to Poznań, tooling warranties, and commissioning.
Upgrade Your Stator Production Cell in Poznań
Connect directly with our engineering division in Dongguan. Forward your stator core drawings (OD, ID, stack height, slot dimensions, and wire diameter) for a complimentary machine recommendation, tooling design review, and DDP/FOB quotation within 9 hours.
