
New Fully Automatic Motor Coil Winding Machine High Quality Coil Maker for Manufacturing Plant Use 220V
220V · Automated Spooling · Dual Flyer
Engineered to handle high-density electromagnetic slot configurations, variable wire calibers (0.1–1.2 mm), and robust single-or-three phase operational requirements across Mexican industrial zones.







Analyzing the strategic imperatives behind electric machine coil winding, brush/brushless DC conversion, and automated production infrastructure within the Mexican industrial corridor.
The industrial polygon of Vallejo in Mexico City, combined with Naucalpan and Tlalnepantla in the State of Mexico (Edomex), has transformed into a critical cluster for Tier-1 automotive and HVAC pump systems. The enforcement of USMCA (T-MEC) regional value content rules requires OEM plants to localize fractional and integral horsepower motor production. Our CNC and multi-spindle winding systems enable sub-assembly operations to slash cycle times while eliminating import dependence on East Asian pre-wound coils.
Toluca, Puebla, and Querétaro supply lines are rapidly shifting from brushed topologies to high-torque Brushless DC (BLDC) and permanent magnet synchronous motors (PMSM) for electronic steering, radiator cooling fans, and regenerative braking actuators. Stator coil winding for these configurations demands precision multi-station internal needle winders (such as our 4-to-6 station series) that precisely lay round enamelled copper without damaging insulation lacquers across narrow slot openings.
CONUEE and Mexican Official Norms (NOM) mandate aggressive minimum energy efficiency standards for alternating current and direct current industrial motors. Traditional manual winding inevitably produces loose slot fill factors and asymmetric end-windings, yielding higher Joule losses and core heat. Deploying automated coil insertion combined with intermediate and final stator coil forming guarantees tight volumetric copper density and reduced parasitic resistance.
A standardized operational matrix mapping hardware tooling, functional automation, and engineering inputs required by plant managers in Mexico City.
| Stage | Manufacturing Step | Assigned Machine Series | Operational Function & Tolerances | Required Tooling Data from Client |
|---|---|---|---|---|
| Step 01 | Slot Cell Insulation | HONGFANG HF-D50 / Wedge Paper Inserter | Feeds, creases, cuts, and pushes dielectric DMD/Nomex insulation paper into lamination slots to eliminate ground faults. | Lamination stack height, slot profile geometry, insulation paper thickness (mm). |
| Step 02 | Precision Coil Winding | CNC Auto Winder / 4-Station Internal Winder | Winds Grade 2 polyurethaned copper/aluminum magnet wire into predetermined coil pitches at speeds up to 3000 RPM. | Wire gauge (0.1–1.2mm), turns per phase, internal stator diameter (ID), pole count. |
| Step 03 | Coil & Wedge Insertion | Automatic Coil & Wedge Inserter | Transfers wound coils and slot closing wedges in a synchronized push stroke to prevent winding abrasions. | Stator outer/inner diameter (OD/ID), wedge material profile, core slot opening width. |
| Step 04 | Intermediate Coil Forming | Stator Coil Forming Machine | Expands and pre-shapes coil end-turns outward to guarantee rotor bore clearance prior to binding. | Bore clearance minimum, coil end-turn height allowance, frame clearance. |
| Step 05 | End-Turn Coil Lacing | HF-BS20 Servo Double-Side Lacing Unit | Servo-driven needles bind coil ends with polyester filament cord to prevent vibrational fatigue and electromagnetic hum. | Single/double side requirement, stitch pitch interval, tension specifications. |
| Step 06 | Final Coil Dimensioning | Hydraulic Stator Coil Forming Press | Final hydraulic calibration ensuring head dimensions meet rigorous motor end-bell assembly tolerances. | Final envelope drawing, housing boundary clearance, terminal lead route. |
| Step 07 | Rotor Surface Turning | HF-C60 Rotor Turning & Cutting Lathe | Micro-cuts rotor core outer surface to maintain uniform air-gap clearances (0.2–0.4mm), preventing magnetic eccentricity. | Rotor lamination stack length, finished OD dimension, concentricity limits (±0.01mm). |
| Step 08 | Shaft Press Insertion | Electric Motor Rotor Shaft Pressing Unit | Interference-fits SC45 carbon steel shafts into core assemblies under calibrated force feedback to avoid bend strain. | Shaft press interference fit (microns), total core press tonnage required. |
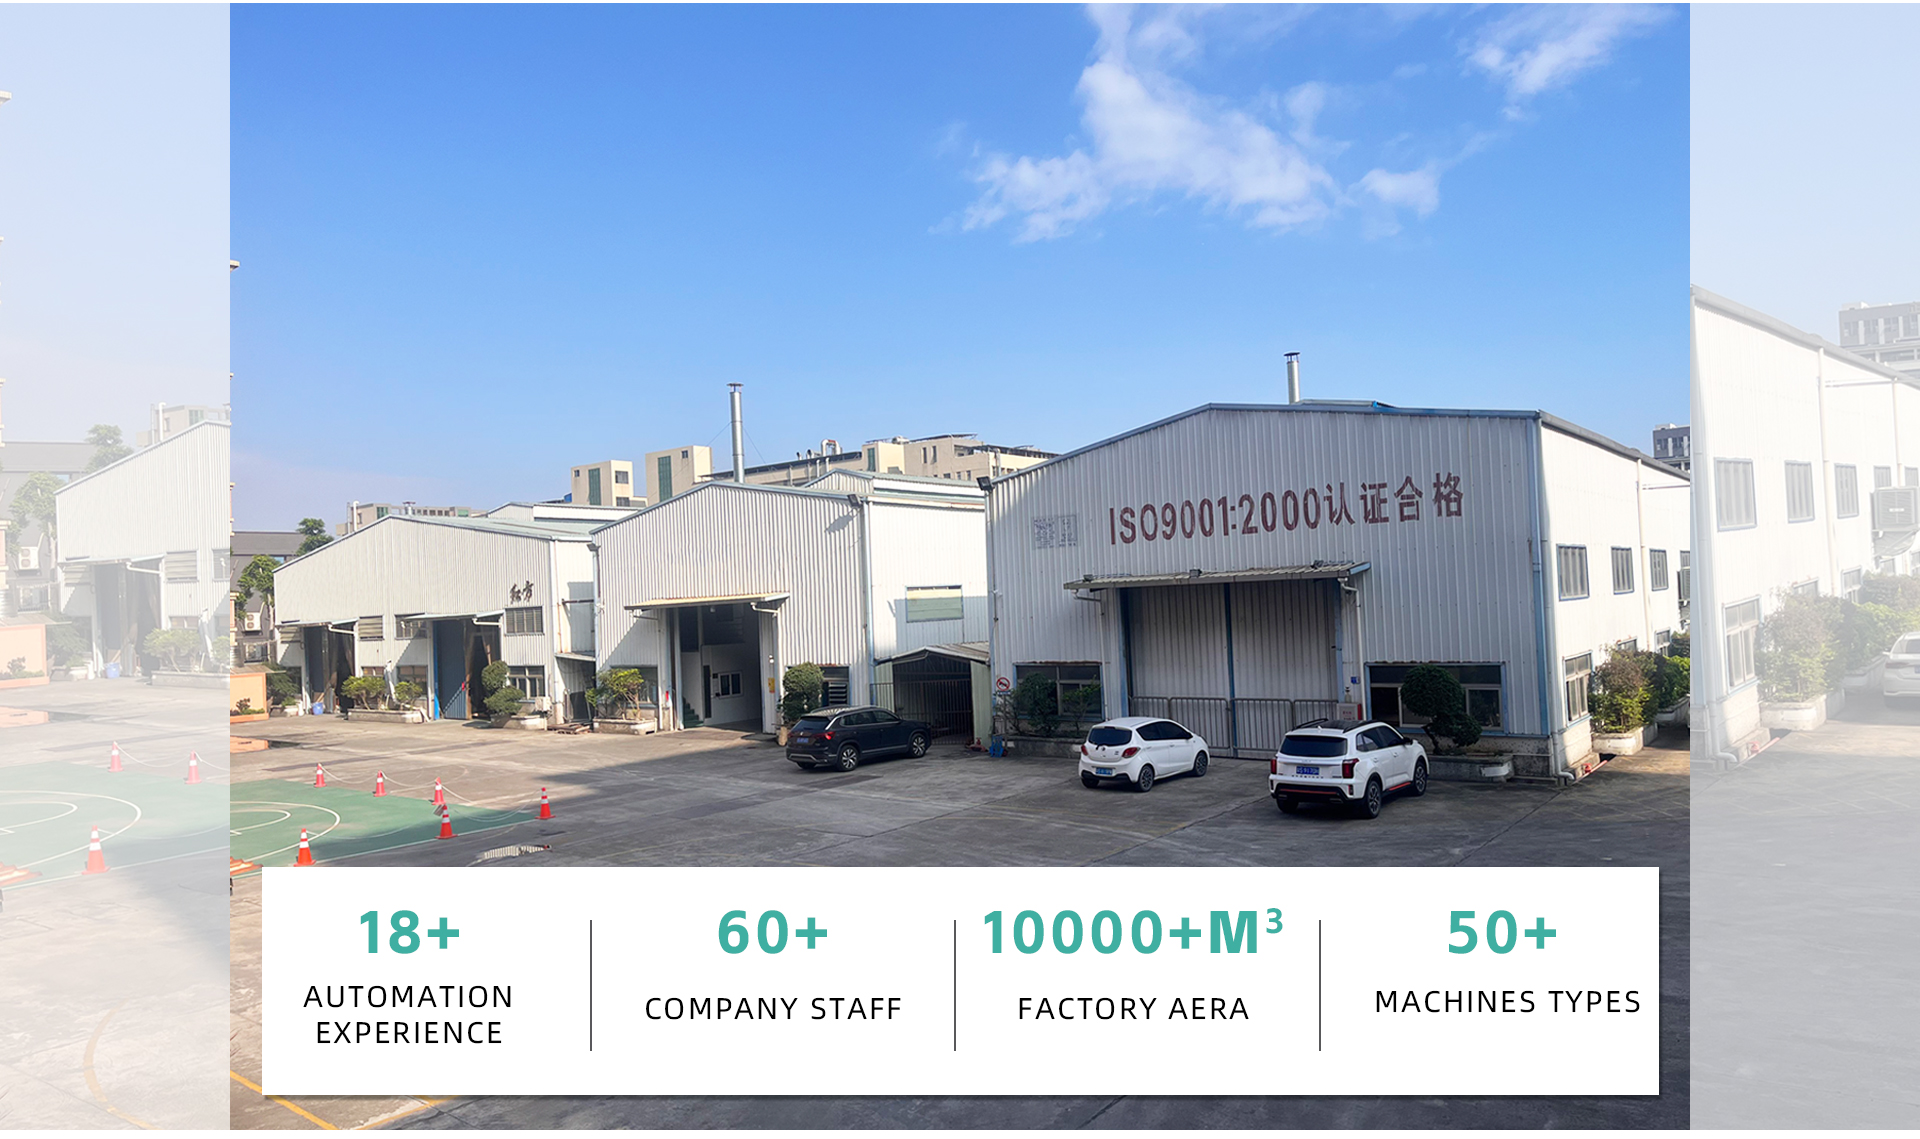
Operating from Qishi Town, Dongguan—the epicenter of global electro-mechanical equipment fabrication—Zunqi Intelligent Equipment Co., Ltd. combines 17 years of direct international export execution with factory-floor customization.
Unlike trading intermediaries, we design and machine core coil formers, insertion fingers, and indexing dials in-house. We bridge the gap between low-tier standard machines and exorbitantly priced European tooling lines, empowering Mexican assembly plants to achieve world-class automation at rapid capital payback periods.



Transparency from blueprint to container loading. Explore our audited workshop environments and precision calibration bays.
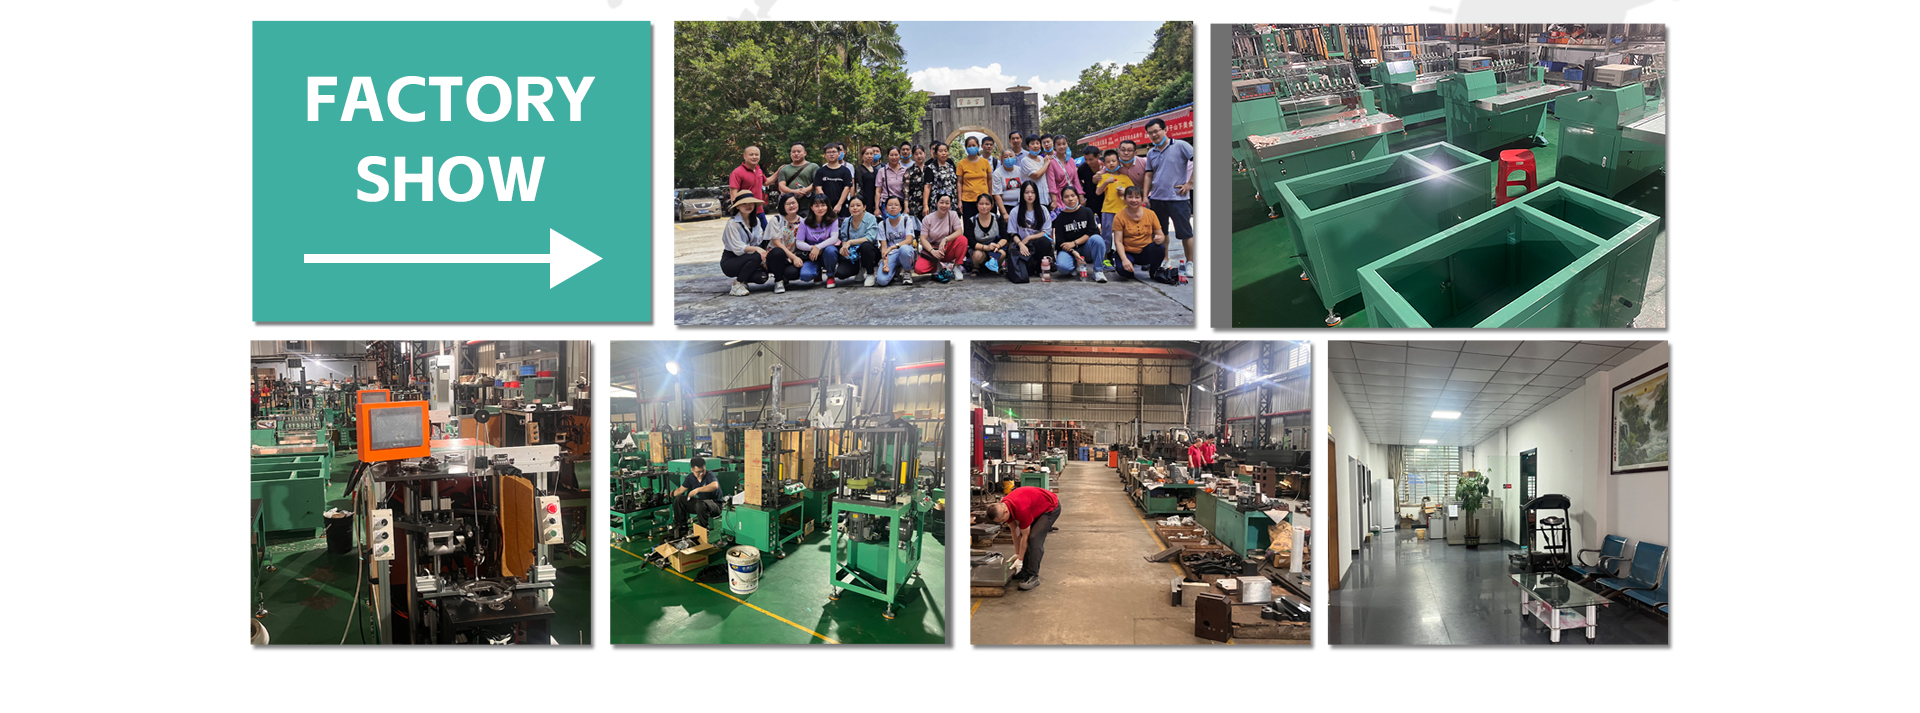
Addressing voltage, customs import protocols (Pedimento Aduanal), maintenance support, and custom tooling turnarounds.
Yes. All machines exported to Mexico City, Guadalajara, or Monterrey are wired natively to your plant's grid specifications: 220V single-phase or three-phase 60Hz, or 440V 60Hz. We calibrate servo drives, PLC transformer taps, and pneumatic frequency cycles to Mexican nominal industrial standards before dispatch.
We supply full export documentation compliant with SAT (Servicio de Administración Tributaria) and Mexican customs broker (Agente Aduanal) requirements. This includes detailed Commercial Invoices, Packing Lists with HS Codes (e.g., 8479.81 for winding machinery), and Certificates of Origin. Machines are crated in solid, fumigation-free plywood meeting ISPM-15 international sea-freight standards.
Standard frames are manufactured within 20–30 business days. Custom tooling tailored to your stator core lamination drawing (OD, ID, stack height, slot profile) requires 10–15 days of CNC electro-discharge machining and heat treatment. Prior to dispatch, we record a physical winding test using your exact wire diameter and slot liner thickness for final approval.
Every equipment shipment includes a complete vulnerable wear-and-tear kit: wire guides, tensioner ceramic eyelets, cutting blades, inserting fingers, and pneumatic seals. For technical support, our bilingual engineering group provides prompt video-assisted diagnostic calls within 9 hours, directly aligned with Central Standard Time (CST / CDMX).
Yes. Our multi-head and flyer winding machinery includes active electronic tensioners with polished ceramic and tungsten-carbide rollers. This avoids peeling the oxide film or necking ductile aluminum wire while providing sufficient tension for heavy-gauge copper winding.
Our minimum order quantity is 1 complete set for any winding, inserting, forming, or rotor turning machine. All equipment includes a comprehensive 12-month factory warranty covering PLC processors, motors, structural frames, and pneumatic components, with rapid courier dispatch of replacement elements.
Send your stator or armature CAD drawings today. Our senior tooling engineers will calculate cycle times, recommend machine configurations, and provide a full technical proposal within 9 hours.
Get Catalog